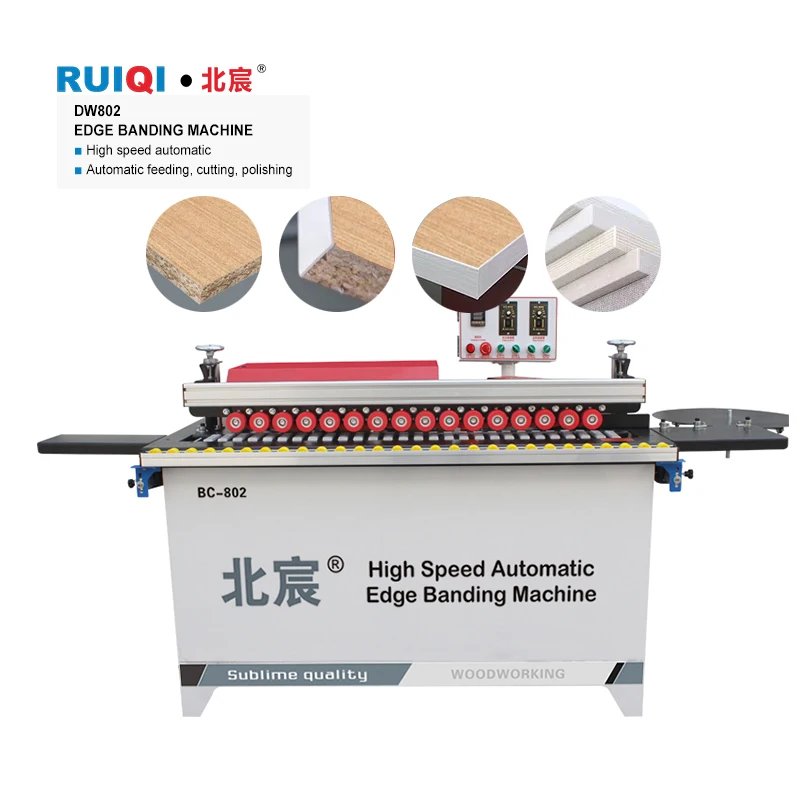
Edge banding machine
Click to enlarge
ISO 9001
CE Certified
OEM / ODM
12-Mo Warranty
Edge banding machine
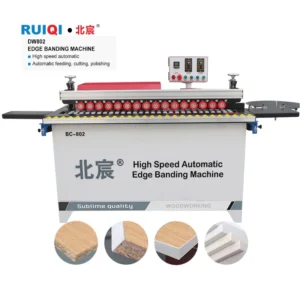
DW802 Automatic Edge Banding Machine for MDF Panel – Process and Application Guide
<p><strong>DW802 Automatic Edge Banding Machine, 220V/380V, 0.3–3 MM Edge Thickness, 4000 ml Glue Pot</strong> — performs gluing, end-cutting, trimming and polishing in a single pass on MDF, particleboard and plywood. Dual 800W trimming and 180W polishing stations deliver clean edge profiles suitable for tight-tolerance cabinet assembly, while the integrated 1200W vacuum keeps melamine surfaces free from chip contamination.</p> <p>Supported by four-stage QC with pre-shipment verification, engineer-led configuration within 24 hours, and full voltage and language customization to match your workshop requirements.</p>
100+
Countries
MOQ 1
Unit
15-25 Days
Lead Time
Automatic Edge Banding
DW802
Edge Banding Machine
MDF Panel
Process And Application Guide
Vacuum System
- Full OEM/ODM support -- custom logo, voltage (110V-440V), multilingual panels
- ISO 9001 & CE certified, 5 national patents, 60 professional engineers
- 12-month warranty, remote technical support & spare parts service
- Professional export packaging, customs clearance support, on-time delivery
Verified Substrate Process Match — every configuration is confirmed against your actual panel material and banding thickness before the machine leaves the factory.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | DW802 |
| Product Type | Automatic Edge Banding Machine |
| Total Power | 4200W |
| Voltage & Frequency | 220V / 380V / customization (frequency to be confirmed) |
| Overall Dimensions (L×W×H) | 130 × 60 × 95 cm |
| Net Weight | 135 kg |
| Minimum Sheet Length | 25 cm |
| Minimum Sheet Width | 10 cm |
| Edge Banding Height | 0–50 mm |
| Edge Banding Thickness | 0.3–3 mm |
| Trimming Power | 800W × 2 |
| Polishing Power | 180W × 2 |
| Glue Pot Capacity | 4000 ml |
| Vacuum Power | 1200W |
| Air Supply Requirement | 0.4–0.8 MPa |
| Key Features | Edge banding, automatic head-and-tail cutting, trimming, polishing, integrated vacuum extraction |
Application Suitability
| Application | Material or Output |
|---|---|
| Cabinet carcass edge sealing | Melamine-faced MDF and particleboard |
| Custom joinery small-batch runs | Ecological board and plywood panels |
| Home decoration workshop production | Solid wood boards with PVC or veneer banding |
| Small furniture component finishing | Offcuts down to 25 cm length |
Why Glue Line Visibility Varies Across Substrates — and What the edge banding machine process and application Must Address
Different substrates absorb and release heat at different rates, changing how the adhesive bonds before it cures.
Melamine-faced particleboard behaves differently from raw MDF or plywood. The resin coating on melamine slows heat transfer into the glue, so the adhesive stays open longer on one side while bonding instantly on the other. Plywood, with its layered grain structure, creates uneven pressure points along the edge that a single trimming pass cannot always clean up. When a workshop switches panel materials without adjusting glue temperature or feed speed, visible glue lines and edge lift become common rejects on the assembly floor [NEED_CITE: substrate-specific adhesive behaviour in panel edge banding].
Glue Behaviour Across MDF, Particleboard and Plywood
The 4000 ml glue pot on this machine provides enough adhesive volume for continuous runs across mixed panel batches. MDF edges are porous and draw glue in quickly, meaning the bond forms fast but the visible squeeze-out needs controlled temperature to avoid staining the surface. Particleboard is less absorbent, so the glue sits longer on the edge before setting — a slower feed speed helps it penetrate the substrate structure. Plywood layers can separate under trimming pressure if the glue has not fully cured, making the dual polishing stations important for final edge cleanup.
Trim Quality and Its Effect on Downstream Assembly
Edge trimming directly determines whether panels fit square during cabinet assembly. The dual 800W trimming stations on the DW802 allow a rough trim followed by a finish pass, which matters when you are running 0.3 mm PVC on one batch and 3 mm veneer on the next. Veneer is brittle and chips easily under aggressive trimming, so the second station operates at a finer cut depth. The integrated 1200W vacuum system removes chips from the trimming zone before they can become trapped under the polishing wheels, which would otherwise leave scratch marks on the finished edge [NEED_CITE: trimming station configuration impact on edge finish grade].
How Core Parameters Shape the Edge Finish You Actually Get
The minimum sheet length of 25 cm and minimum width of 10 cm determine what offcuts from a panel saw can be fed through this machine. For a cabinet maker producing narrow drawer sides or small shelf brackets, these limits define whether an automated edge bander can replace manual banding on every component. The 0–50 mm edge banding height range covers standard 16 mm and 18 mm cabinet panels as well as thicker worktop sections. Air supply between 0.4 and 0.8 MPa drives the pneumatic pressure rollers — running below 0.4 MPa reduces roller contact force and creates uneven glue distribution, particularly noticeable on longer panels. The total power draw of 4200W means the machine can operate on a standard workshop circuit without requiring a dedicated high-capacity line.
What Happens When the Machine Configuration Ignores Your Panel Mix
A workshop that buys an edge bander based only on maximum feed speed often discovers the problem weeks after delivery. If the glue pot is undersized for your batch volume, operators stop to refill mid-run and the adhesive cools unevenly in the pot. If the trimming stations lack sufficient power for your banding thickness, the rough trim leaves ridges that the polishing stage cannot remove. Panels arrive at the assembly bench with visible edge defects, and the carpenters spend time sanding edges that should have been machine-finished [NEED_CITE: common edge banding defects from configuration mismatch].
Why Procurement Through This Channel Reduces Setup Risk
The engineering team reviews your panel material, banding type and daily volume before proposing a configuration, so the machine arrives matched to your actual process rather than a catalogue default. Voltage is confirmed against your facility supply before production begins, preventing the commissioning failure that occurs when a 380V machine arrives at a 220V-only workshop. Control panel language is set to match your operators, avoiding stalled installations where no one can read the display. The four-stage quality check includes a pre-shipment test run on material matching your specification, and the results are documented before the machine is crated.
Documentation & Verification
- CE declaration of conformity covering the DW802 electrical and mechanical safety requirements
- Machine specification sheet listing confirmed voltage, frequency and trimming station power values
- Electrical schematic matched to your facility supply for local electrician review before arrival
- Factory test record showing edge banding results on your specified panel material and banding thickness
- Operation and maintenance manual written in your operator’s language with pneumatic system diagrams
- Spare parts list identifying trimming blades, polishing wheels and glue pot seals by part number
Installation, Commissioning & Support
- Requires a level floor area accommodating the 130 × 60 cm footprint with clearance for panel infeed on both sides
- Electrical connection must match confirmed voltage with a dedicated circuit rated above the 4200W total power draw
- Pneumatic line must deliver 0.4–0.8 MPa clean dry air to the machine inlet for consistent roller pressure
- First-run commissioning includes glue temperature calibration against your specific panel substrate and banding material
- Operator training covers trimming station adjustment for switching between PVC and veneer within the 0.3–3 mm range
- Routine maintenance schedule for glue pot cleaning, vacuum filter replacement and polishing wheel dressing
What We Need From You Before Quoting
Tell us which panel substrates you run most often — MDF, particleboard, plywood or a mix — and what edge banding material and thickness you typically apply. Confirm your workshop voltage and frequency so the electrical system is built correctly before dispatch. If you have panels that have shown glue line problems in the past, send a sample or a photograph so the process parameters can be adjusted before your machine ships.
Frequently Asked Questions
Q: How does edge banding quality vary across MDF, particleboard and plywood substrates?
A: MDF absorbs glue quickly due to its porous edge, so temperature must be controlled to prevent surface staining. Particleboard holds glue on the surface longer, requiring slower feed speed for penetration. Plywood layers create uneven pressure along the edge, making the dual polishing pass important for a clean finish. The edge banding machine process and application settings must account for each substrate’s heat transfer behaviour.
Q: Which PVC and veneer thicknesses work best within the 0.3–3 mm range?
A: Thin PVC around 0.4 mm is forgiving on curved edges and trims cleanly at standard feed speeds. Thicker veneer up to 3 mm requires slower feed and lighter trimming pressure to prevent chipping along the grain. Banding material choice affects how the two trimming stations are set — veneer needs a finer second pass, while PVC tolerates more aggressive rough trimming without edge damage.
Q: How do trimming and polishing stations affect final assembly tolerances?
A: The dual 800W trimming stations remove excess banding in two stages, leaving a square edge that mates cleanly with adjacent panels during cabinet assembly. The polishing stations then smooth the trimmed edge to remove any micro-ridges. If trimming leaves even a slight lip, panels will not sit flush against each other, creating visible gaps in assembled carcass interiors.
Q: What do the minimum panel dimensions mean for small offcut processing?
A: The 25 cm minimum length and 10 cm minimum width allow narrow drawer sides, shelf brackets and other small components to be edge-banded automatically rather than manually. This matters in custom cabinet production where a single sheet yields several small offcuts that still need finished edges. Panels below these dimensions cannot be fed through the pressure roller system reliably.
Q: How does the integrated vacuum system influence edge cleanliness?
A: The 1200W vacuum extracts chips and adhesive offcuts directly from the trimming zone before they reach the polishing wheels. Without this extraction, trapped particles get pressed into the fresh glue line during polishing, creating visible marks especially on light-coloured melamine-faced panels. Clean extraction keeps the glue line invisible on finished cabinet interiors where edges are exposed to view.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Name | DW802 Automatic Edge Banding Machine for MDF Panel – Process and Application Guide |
| Category | Edge banding machine |
| Voltage Options | 110V / 220V / 380V / 440V (customizable) |
| Frequency | 50Hz / 60Hz (customizable) |
| Certification | ISO 9001, CE |
| MOQ | 1 Unit |
| Lead Time | 15-25 Working Days |
| Warranty | 12 Months |
| OEM / ODM | Available -- logo, color, panel language |
* Detailed technical specifications vary by model. Please contact us with your specific requirements for a complete datasheet.
Shipping & Export
-
Export Packaging
Heavy-duty wooden crate with foam padding and moisture protection
-
Shipping Methods
Sea freight (FCL/LCL), air freight, express -- we support all methods
-
Customs Support
Full documentation: CO, commercial invoice, packing list, HS code assistance
-
Port of Loading
Tianjin / Qingdao port, China -- 20 years export experience
OEM / ODM Services
-
Logo & Branding
Custom logo printing, color scheme, and nameplate engraving
-
Voltage Configuration
110V / 220V / 380V / 440V, 50Hz / 60Hz -- any region supported
-
Multilingual Panels
Control panels in English, Spanish, French, Arabic and more
-
Custom Specifications
Modified dimensions, accessories, or feature sets on request
Get a Quote
Request Product Inquiry
Fill in your details and we'll respond within 24 hours with pricing and availability.
Direct Contact
How It Works
-
1
Confirm requirements & budget
Tell us your factory scale and processing needs
-
2
Receive recommendation & quote
We match the right machine with full specs
-
3
Negotiate & place order
OEM terms, voltage, payment and delivery
-
4
Production & QC inspection
Multi-stage quality control by 60 engineers
-
5
Export packaging & shipment
Professional packing, customs clearance
-
6
After-sales support
12-month warranty, remote tech support
You May Also Like